


Brief Introduction:
POLYCIMA-5002G15 reinforced polypropylene is a glass fiber reinforced polypropylene material. It adopts unique processing technology to ensure the length of glass fibers as well as their dispersion and distribution in the PP matrix. The bonding between the glass fibers and the PP matrix is excellent. Therefore, POLYCIMA-5002G15 reinforced polypropylene features high strength, high toughness, good flowability for product processing, and low warpage and deformation.
Main Applications:
Electronic and electrical products, building industry products, etc.
Performance Indicators
Performance | Test Method | Unit | 5002G15 |
Density | ASTM D 792 | g/cm³ | 1.05 |
Melt Flow Index (230°C/2.16kg) | ASTM D 1238 | g/10min | 8.0 |
Tensile Strength | ASTM D 638 | MPa | 80 |
Elongation at Break | ASTM D 638 | % | 15 |
Flexural Strength | ASTM D 790 | MPa | 95 |
Flexural Modulus | ASTM D 790 | MPa | 3700 |
Izod Notched Impact Strength | ASTM D 256 | J/m | 75 |
Heat Deflection Temperature (0.46MPa) | ASTM D 648 | °C | 155 |
Injection Molding Process
Drying Temperature/Time | Injection Temperature | Injection Speed | Mold Temperature |
90℃/2H | 220-190℃ | 50-80% | 40-70℃ |
Packaging/Storage:
25kg/bag; transport as general chemical product. Store in a dry, cool place, away from direct sunlight.
Note:
The physical property technical indicators and data provided in this document are for reference only and cannot be used as a basis for inspection or guarantee. Users who purchase our products are also responsible for conducting experiments to verify whether they are suitable for their intended processes, applications, performance requirements, and standards. Since the application and processing of our products are beyond our control, any issues arising during such use shall be solely the responsibility of the user.
Molding Processing Guide
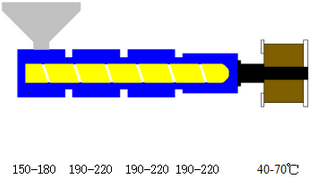
Screw Temperature (°C):
Processing Main Considerations:
A: It is recommended to dry at 90°C for 2–4 hours.
B: It is recommended to clean the screw or die with polypropylene or polyethylene before and after processing this material.