


Product Description:
POLYCIMA-80Q98F is a low-smoke zero-halogen (LSZH) polyolefin material based on inorganic flame retardants. It meets the requirements of regulations such as RoHS, SVHC, 16P, and PAHs, and exhibits excellent mechanical and physical properties, electrical properties, and processing characteristics.
Product Applications:
It can be used in optical fiber drop cables, sheaths, wire insulation and sheaths, etc. Extrusion methods include pressure extrusion, semi-tube extrusion, and tube extrusion. Some products can also be injection molded. Compared with similar products from other manufacturers, it offers stable flame retardancy, a finer surface appearance, and better scratch resistance.
Property | Test Method | Unit | Typical Value |
Density | GB/T1033-1986 | g/cm³ | 1.48 |
Tensile Strength | GB/T1040-1992 | MPa | 12.3 |
Elongation at Break | GB/T1040-1992 | % | 165 |
Aging Performance | GB/T2951.2-1997 | °C × h | 100 × 168 |
Tensile Strength Retention | GB/T2951.2-1997 | % | ≥75 |
Elongation at Break Retention | GB/T2951.2-1997 | % | ≥75 |
Brittleness Temperature (Low Temp. Impact) | GB/T5470 | °C | -25 |
Smoke Density (Flaming method) | - | - | 90 |
Smoke Density (Non-flaming method) | - | - | 235 |
Toxicity Index | - | - | 0.8 |
pH Value | IEC60754-2 | - | 5.2 |
Electrical Conductivity | - | μS/mm | 0.48 |
Dielectric Strength | GB/T1408 | kV/mm | 25 |
Oxygen Index | ISO4589-2 | % | 32 |
Packaging/Storage:
25 kg/bag. Transport as general chemical product. Store in a dry, cool place away from direct sunlight. Shelf life: 1 year.
Note:
The technical property indicators and data provided in this document are for reference only and cannot be used as a basis for inspection or guarantee. Users who purchase our products are also responsible for conducting their own tests to verify whether the product is suitable for their intended processes, applications, performance requirements, and standards. Since the application and processing of our products are beyond our control, any related issues shall be solely the responsibility of the user.
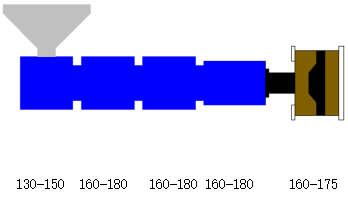
Injection Molding Guidelines:
· Shrinkage: 0.010–0.020 inch
· Injection Speed: Medium–Fast
· Injection Pressure: Medium–High
· Back Pressure: Low–Medium
· Holding Pressure: Sufficient for product shaping inside the mold
· Cooling: Sufficient for product demolding
· Screw Temperature (°C):
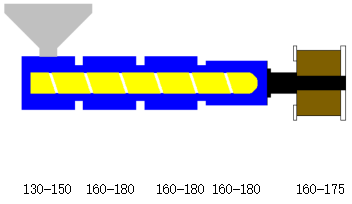
Extrusion Processing Guidelines:
· Length/Diameter Ratio: 20:1–25:1
· Compression Ratio: 1.5–2.3
· Breaker Plate and Screen Pack: Required
· Draw Down Ratio: 5–10%
· Cooling: Water Bath Cooling
· Screw Temperature (°C):
Processing Precautions:
A: It is recommended to dry the material at 90°C for 2–4 hours.
B: It is recommended to clean the screw and die head using a special purging compound before and after processing this material.